Germany
Outfield Gantry Crane
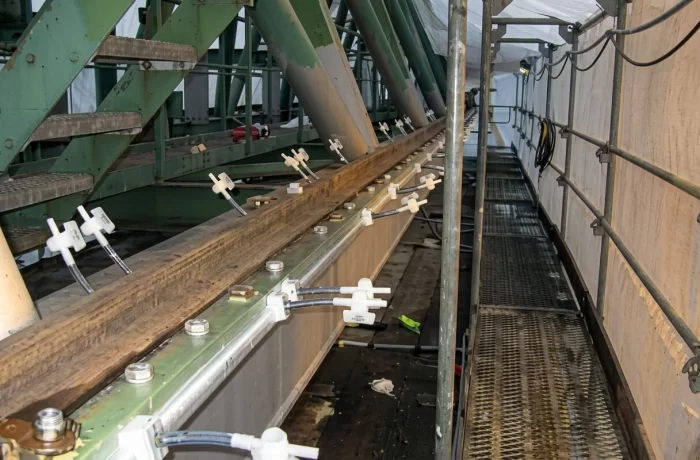
Refurbishment of a wavy, tilted crane rail on a 90 m-span structure, restoring safe transportation of loads up to 32 tonnes after the original rail support could no longer maintain alignment.
Full-surface, force-fit connection between rail support and steel girder.
Fatigue-tested to 10 million load cycles at ibac RWTH Aachen.
A crane runway rail carries dynamic wheel loads for the structure’s full service life. Grouting compounds aren’t adequately designed for this application, especially where rail slats sit on a steel girder instead of concrete.
DIAMANT MM1018 closes that gap with a full-surface, force-fit layer, fatigue-tested to 10 million load cycles and proven in crane rail refurbishment projects worldwide.
Kubri Engineered Solutions is the Australian technical partner for DIAMANT Polymer GmbH, supplying and specifying MM1018 for overhead crane, gantry crane, and port crane runway rail installations and refurbishment.
Grouting compounds like cement, polyester, or epoxy resin mortar are standard for casting under crane rail supports onto concrete. But when the rail slats sit on a steel girder or floor plate instead, the requirements are usually either too high or insufficiently defined for standard grouting compounds to meet.
Gaps of less than 2mm can make simple grouting impossible outright. Where the connection can be grouted, low creep performance to protect preload in the fastening screws is as much a requirement as the coefficient of friction the connection needs to carry under load.
A crane runway rail doesn’t present a static load case, either. It sees dynamic wheel loads on every pass and for every load the crane lifts, over the structure’s full service life.
Left unaddressed, crane rails become deformed under high loads over time, a predictable outcome of a static grouting solution applied to a genuinely dynamic, fatigue-governed connection.
MM1018 is a two-component polymer that fills gaps below 2 mm and cures into a load-bearing layer engineered for the friction and low-creep performance a steel-to-steel rail connection needs- two requirements standard grout struggles to meet on this connection type.
MM1018 FL or P is poured, injected, or trowelled into the gap between the crane rail support and the steel girder or floor plate beneath it. It flows into the geometry and cures into a dimensionally stable layer that restores a permanent, precise connection between the rail support and the structure, in a four-step sequence carried out on site:
01
the gap perimeter is sealed with MM1018 Seal, using its fast-curing, corrosion- and weather-resistant properties to create a pressure-tight joint seal before injection begins.
02
MM1018 FL is poured or injected into the gap, or MM1018 P is applied by trowel where the connection is vertical, or the material needs to be positioned precisely, with injection and ventilation points planned so trapped air is displaced ahead of the material.
03
The material cures with negligible shrinkage (0.035%) and reaches ≥97% of design strength at 24 hours (+21°C) with full design strength at 7 days. Service load is not to be applied before strength is verified.
04
Sample sets are taken during the pour and checked for Shore D hardness and cure consistency before the rail is loaded and the crane system returns to service.
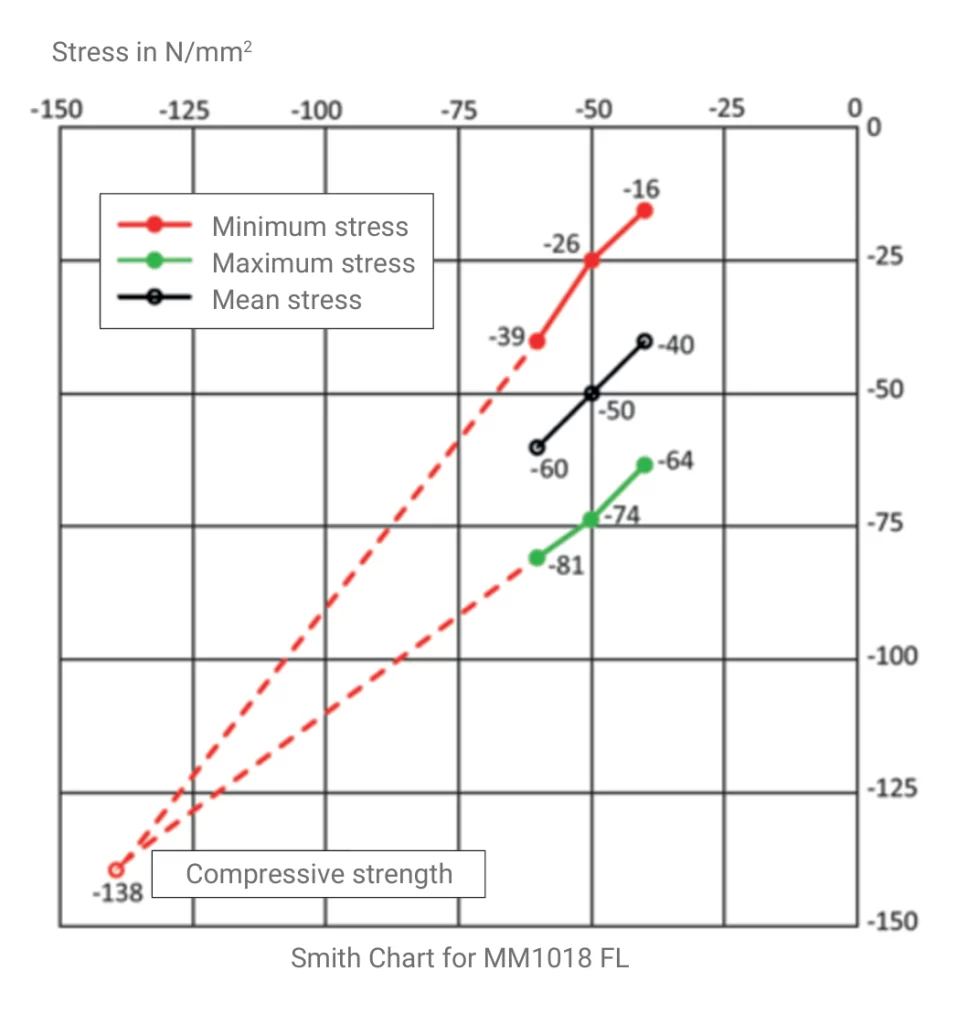
MM1018 FL has been fatigue-tested to 10 million load cycles and has passed. Testing was carried out independently by ibac at RWTH Aachen (test M1999) at mean stresses of 40, 50, and 60 N/mm²; all three test series completed the full 10 million cycles with no loss of structural integrity. For context, EN 1993-1-9 sets the constant-amplitude fatigue limit for structural steel at 5 million cycles.
DIAMANT’s relaxation testing, extrapolated from a 2mm gap under sustained load, documents a ~10% loss of pretensioning force after 50 years. This supports the material’s suitability for prestressed rail support connections where preload retention is critical to keeping the connection tight under repeated wheel load.
MM1018 FL holds German general building authority approval (abZ Z-3.82-2042) from DIBt. It achieves a compressive strength of 161 N/mm² under DIN EN 12190:1998.
| Property | Value |
|---|---|
| Fatigue strength | 10,000,000 load cycles at mean stresses of 40, 50, and 60 N/mm² (ibac RWTH Aachen, test M1999). No loss of structural integrity recorded |
| Compressive strength (fully cured) |
161 N/mm² (DIN EN 12190:1998) |
| Preload force retention | 90% retained (approximately 10% loss) after 50 years under sustained load (2mm gap, log. extrapolated, restrained) |
| Shrinkage | 0.035% (DIN EN 12617-4:2002) |
| Curing time to full load capacity | 97% or more of design strength at 24 hours (+21°C); full design strength at 7 days. Service load not to be applied before strength is verified. |
| Curing at other temperatures | Min. curing temperature +5°C; accelerated curing permitted to a maximum of 50°C. Strength development varies with temperature. Refer to DIAMANT TDS #1866 V1.1 for values by temperature and age. |
| Maximum layer thickness (manufacturer-tested) | Up to 140 mm |
| Maximum layer thickness (abZ-approved) | Up to 10 mm per layer |
| Service temperature (per abZ) |
-20°C to +50°C |
| Product variants for this application | MM1018 FL (injected, horizontal or accessible gaps) and MM1018 P (trowel-applied, vertical or precisely positioned gaps) |
| Key accessories | MM1018 Seal (perimeter sealing), injection/ventilation packers, DIAMANT cleaner, screw protection where applicable |
The compressive strength, fatigue, and preload retention figures for MM1018 are sourced from the official DIAMANT Technical Datasheet (#1866, Version 1.1, dated 14 July 2026).
KES can map this data against project-specific specifications on request, consistent with AS 1418.18.
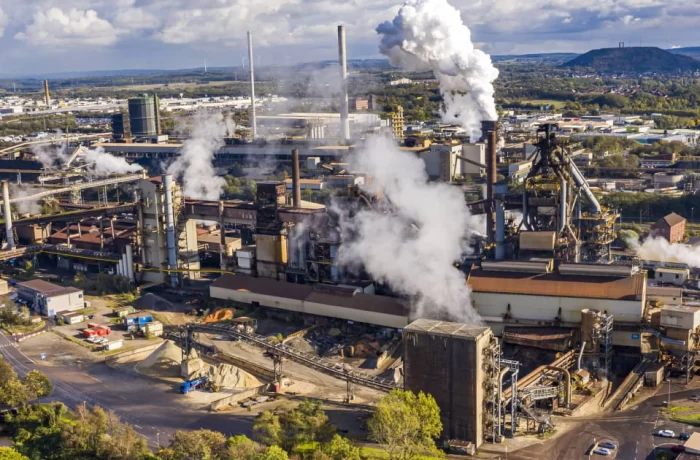
Germany
Refurbishment of a wavy, tilted crane rail on a 90 m-span structure, restoring safe transportation of loads up to 32 tonnes after the original rail support could no longer maintain alignment.
Hamburg, Germany
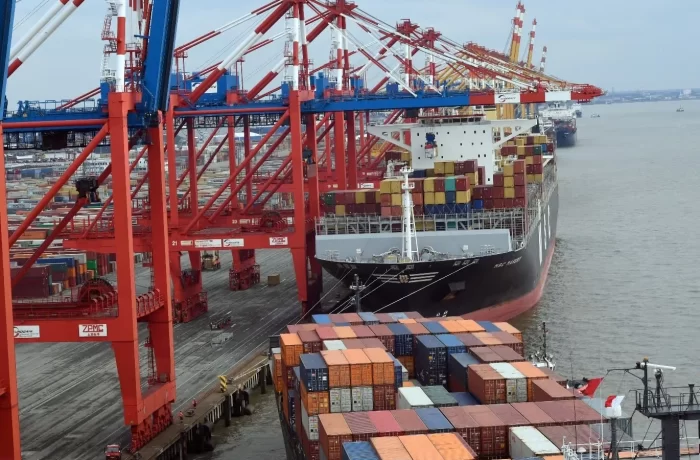
Rail joint refurbishment across 24 container gantry cranes weighing up to 2,100 tonnes and lifting loads of up to 66 tonnes, using MM1018 P to seal gaps between new and existing steel rail sections.
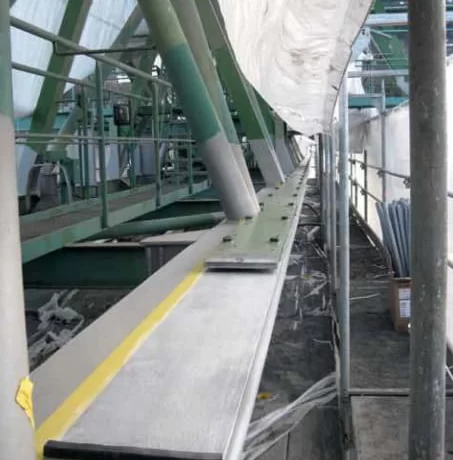
Dillingen, Germany
Refurbishment of an 80-tonne, 36 m-span, 300 m crane runway at Europe's largest plate steel mill, using MM1018.
Germany
Renovation of a 300 m rail track on a crane with an 80-tonne maximum load-bearing capacity, combining new girder slats with MM1018 injection after damage was discovered beneath the removed rail.
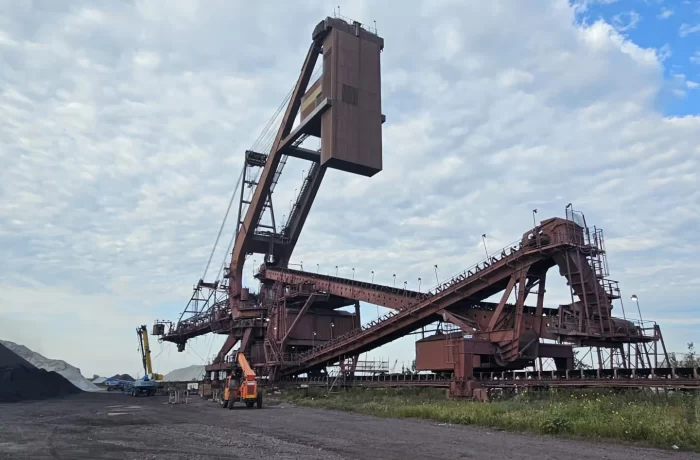
Burns Harbour, USA
Swivel track replacement on a 55-year-old stacker and reloader, refurbished with MM1018 in place of a full track rebuild.
For a full technical overview of liquid shim technology and applications,
visit the Liquid Shim in Australia Resource Centre
For heavier port and marine equipment,
see Liquid Shim for Offshore, Marine, and Heavy Port Equipment
Kubri Engineered Solutions is Australia’s dedicated technical authority for liquid shim technology and the Australian partner for DIAMANT Polymer GmbH, manufacturer of MM1018 The Liquid-Shim®.
KES supports every specification with a complete engineering support package:
Design Support:
Engineering review of the rail support interface during the design phase, before refurbishment commences.
Installation Methodology:
Project-specific method statements, ITP hold points, and on-site attendance for first-of-type crane rail installations.
Interface Control:
Product selection across the MM1018 family (FL, P, Smart S, Seal) matched to gap geometry, access, and shutdown window constraints.
Documentation:
Material certification, batch traceability, abZ approval documentation, and installation records formatted for ITP, handover, and the asset register.
Founded by Loai Shokry, a Chartered Professional Engineer (CPEng) with a career spanning the design and delivery of multi-billion-dollar infrastructure projects in Australia and worldwide, Kubri Engineered Solutions operates as a specification and engineering partner across the full project lifecycle, from design review to handover documentation.
Final product selection and specification remain subject to engineer-of-record approval for your project.
Yes. MM1018 is used in refurbishing existing, often decades-old, weathered steel girder structures by installing a new rail support with a deliberate gap, then filling that gap with MM1018 to achieve precise alignment on both sides of the rail support.
MM1018’s flowable form allows it to fill gaps below 2mm (the point at which standard grouting compounds become impractical) without requiring mechanical processing or adjustment once poured.
DIAMANT recommends grid-blasting to a roughness of 50-60 µm (SA2.5) where practical, and cleaning the surface free of oil, corrosion products, and dust with DIAMANT cleaner or equivalent beforehand.