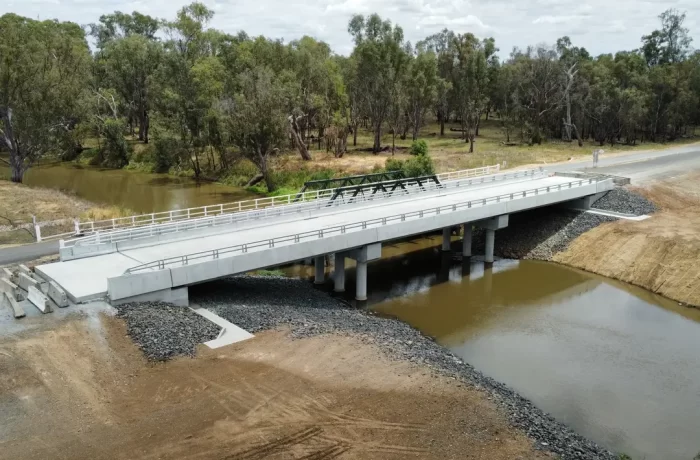
New South Wales, Australia
Warroo Bridge
Existing laminated elastomeric bearings retained and returned to full-area contact via light jacking and MM1018 injection, avoiding a full bearing-replacement programme.
Full-surface load transfer under pot, spherical, elastomeric and disc bearings.
Fatigue-tested to 10 million load cycles at ibac RWTH Aachen.
DIAMANT MM1018 has been carrying bridge bearing loads since 1993, when it was first used in a bearing exchange on a railway bridge in Cologne, Germany. That installation remains in service over three decades later.
Kubri Engineered Solutions is the Australian technical partner for DIAMANT Polymer GmbH, supplying and specifying MM1018 for bearing seat interfaces in new installations and bearing replacement projects alike.
Bridge bearings are designed to spread load evenly across their full footprint, which depends on continuous contact with the seat beneath. However, this contact rarely exists in practice.
Formwork tolerance and curing distortion leave gaps in new structures, and on replacements it’s worse: bearings installed through the 70s and 80s are now approaching or past their intended service life, and forty-plus years of corrosion and pitting have pushed their pedestals further out of plane than the bearing was designed to tolerate.
Over the millions of load cycles a bearing carries across decades of service, that uneven contact leads to seating cracks and progressive rotation. Replacement work compounds the constraint, because a live or staged-traffic shutdown window leaves no time for a slow-curing fix.
Engineers have traditionally closed the gap with individually machined steel lining plates or wedge plates. That approach assumes a known, uniform gap ahead of time, and it still leaves point contact rather than a continuous bearing surface.
MM1018 FL is a liquid, poured or injected into a sealed gap. It flows into the geometry of the seat and cures into a rigid, stable layer that carries load across the bearing’s entire footprint, in a four-step sequence carried out on site:
01
The gap perimeter is sealed with MM1018 Seal, pressed in to a minimum depth for a leak-proof barrier, then left to cure before injection begins.
02
MM1018 FL is injected from the lowest point upward through planned injection and ventilation points so trapped air is pushed out ahead of the material.
03
The material cures with negligible shrinkage (0.035%) and reaches ≥97% of design strength at 24 hours (+21°C) with full design strength at 7 days. Service load is not to be applied before strength is verified.
04
Sample sets are taken during the pour and checked for Shore D hardness and cure consistency before the bearing is loaded.
The method applies to pot, spherical, elastomeric and disc bearings, for both new installation and replacement of an ageing bearing.
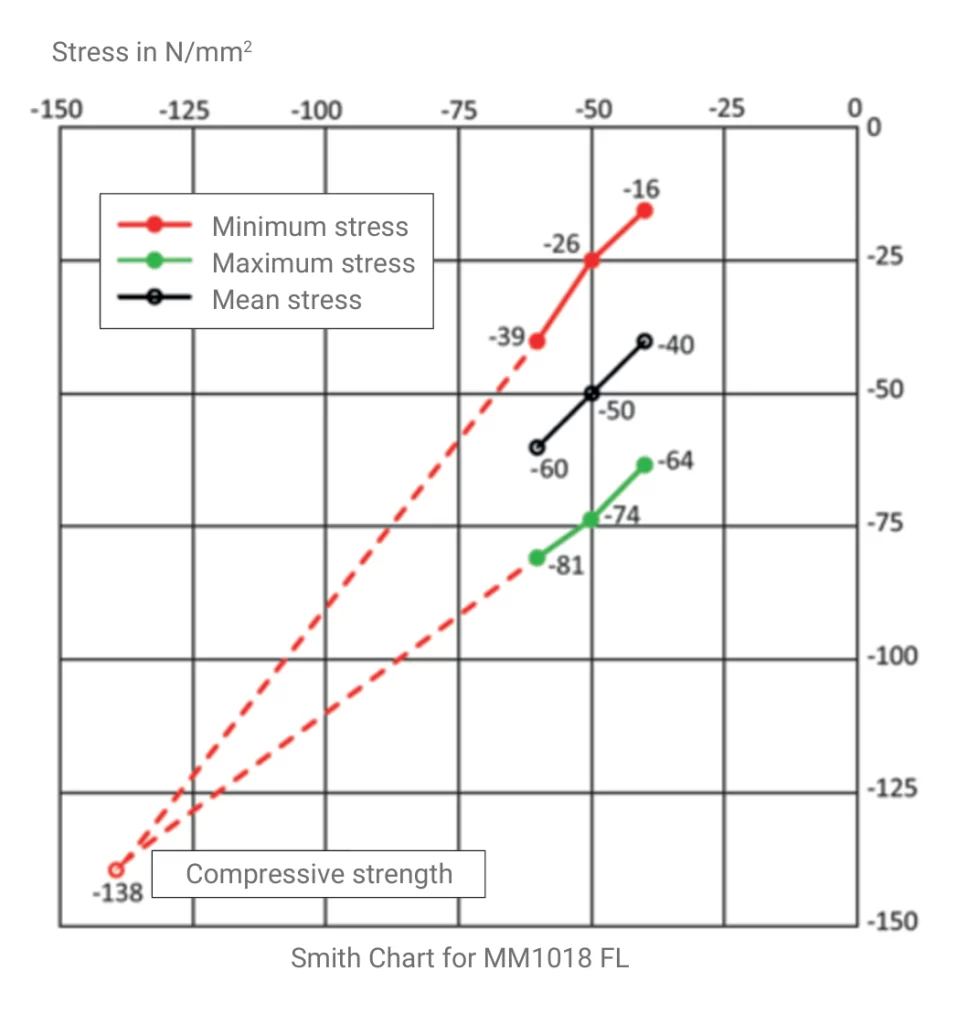
Bridge bearing failure is not the result of a single large load, but from the millionth or ten-millionth repetition of an ordinary one. The most important credential for a bearing seat material is how its compressive strength holds up under repeated loads.
MM1018 FL has been fatigue-tested to 10 million load cycles and has passed. Testing was carried out independently by ibac at RWTH Aachen (test M1999) at mean stresses of 40, 50, and 60 N/mm²; all three test series completed the full 10 million cycles with no loss of structural integrity. For context, EN 1993-1-9 sets the constant-amplitude fatigue limit for structural steel at 5 million cycles.
MM1018 FL holds German general building authority approval (abZ Z-3.82-2042) from DIBt. It achieves a compressive strength of 161 N/mm² under DIN EN 12190:1998.
| Property | Value |
|---|---|
| Fatigue strength | 10,000,000 load cycles at mean stresses of 40, 50, and 60 N/mm² (ibac RWTH Aachen, test M1999). No loss of structural integrity recorded |
| Compressive strength (fully cured) |
161 N/mm² (DIN EN 12190:1998) |
| Curing time to full load capacity | 97% or more of design strength at 24 hours (+21°C); full design strength at 7 days. Service load not to be applied before strength is verified. |
| Curing at other temperatures | Min. curing temperature +5°C; accelerated curing permitted to a maximum of 50°C. Strength development varies with temperature. Refer to DIAMANT TDS #1866 V1.1 for values by temperature and age. |
| Maximum layer thickness (manufacturer-tested) | Up to 140 mm |
| Maximum layer thickness (abZ-approved) | Up to 10 mm per layer |
| Service temperature (per abZ) |
-20°C to +50°C |
| Shrinkage | 0.035% (DIN EN 12617-4:2002) |
| Key accessories | MM1018 Seal (perimeter sealing), injection/ventilation packers, DIAMANT cleaner, screw protection where applicable |
Bridge bearings in Australia are specified and assessed under AS 5100.4.
The fatigue, compressive strength, and durability figures for MM1018 are sourced from the official DIAMANT Technical Datasheet (#1866, Version 1.1, dated 14 July 2026); KES can map this data against project-specific AS 5100 clauses on request.
New South Wales, Australia
Existing laminated elastomeric bearings retained and returned to full-area contact via light jacking and MM1018 injection, avoiding a full bearing-replacement programme.
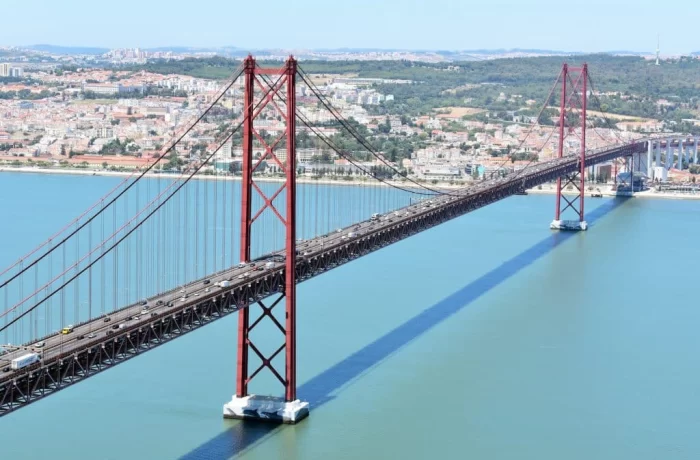
Lisbon, Portugal
500 bridge bearings replaced under live road and rail traffic, with the project completed in approximately 167 hours at roughly 20 minutes per bearing.
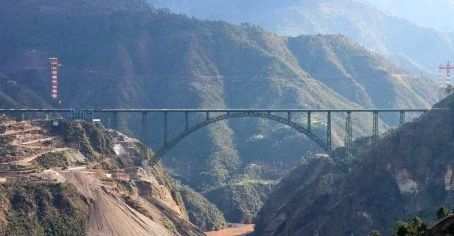
Jammu & Kashmir, India
Arch base plate foundation and bearing installation on the world's highest railway bridge; more than 150 bearings installed with MM1018.
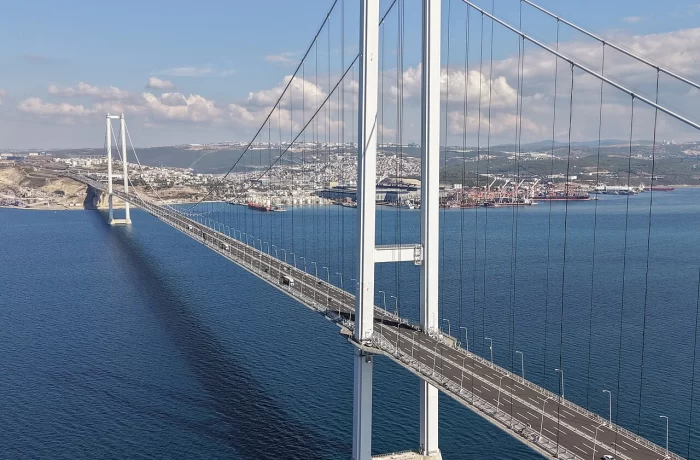
Kocaeli, Turkey
Bearing installation of all elastomeric bearings of the foreland bridge, more than 200 bearings.
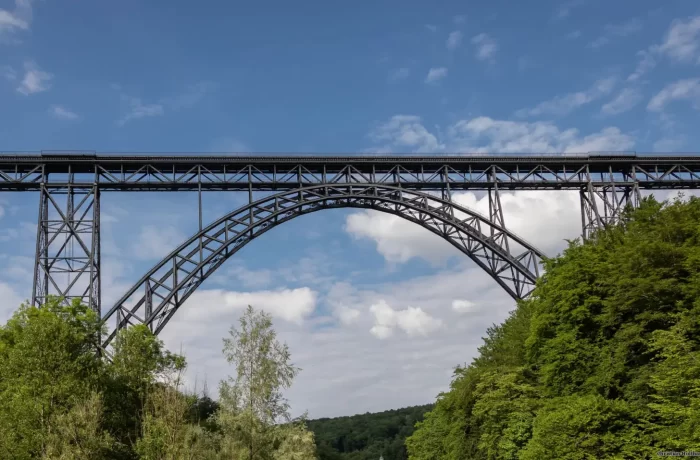
Solingen, Germany
Complete reconditioning of Germany's highest railway bridge; all 80 bearings installed with MM1018.
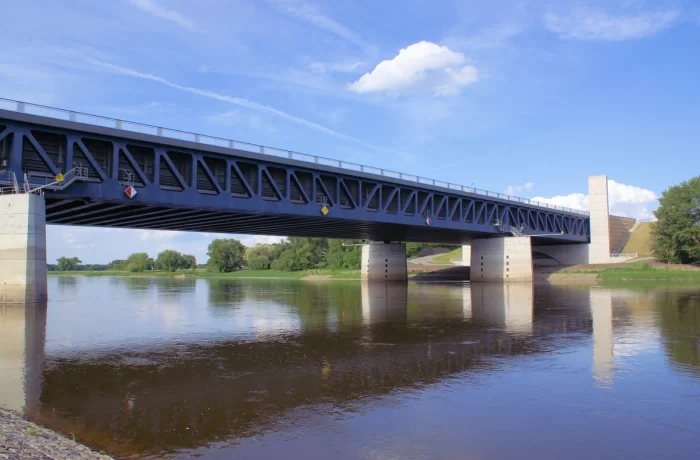
Magdeburg, Germany
Channel-crossing bridge connection for the heaviest steel building in Europe; 4×4m pot bearings installed with MM1018 liquid shim.
For a full technical overview of liquid shim technology and applications,
visit the Liquid Shim Australia resource centre.
Kubri Engineered Solutions is Australia’s dedicated technical authority for liquid shim technology and the Australian partner for DIAMANT Polymer GmbH, manufacturer of MM1018 The Liquid-Shim®.
KES supports every specification with a complete engineering support package:
Design Support:
Interface review and product-variant selection (FL, P, or Smart S) matched to the gap geometry and load case. We resolve the correct specification before steel is fabricated.
Installation Methodology:
Project-specific method statements, ITP clauses, QA hold points, and on-site first-of-type attendance where required. The method is engineered, not improvised.
Interface Control:
Selection across the full MM1018 product family: FL, P, Smart S, MM1018 SEAL, EP-Flow, and the complete DIAMANT injection hardware system, matched to gap geometry and project constraints.
Documentation:
Material certification, batch traceability, abZ approval documentation, ibac fatigue test report, and installation records formatted for ITP, project handover, and asset register.
Founded by Loai Shokry, a Chartered Professional Engineer (CPEng) with a career spanning the design and delivery of multi-billion-dollar infrastructure projects in Australia and worldwide, Kubri Engineered Solutions operates as a specification and engineering partner across the full project lifecycle, from design review to handover documentation.
Final product selection and specification remain subject to engineer-of-record approval for your project.
Yes. MM1018 FL is poured or injected into the sealed gap between the bearing and its seat, whether that seat is a new concrete pour (Osman Gazi Bridge) or an existing, aged pedestal (Ponte 25 de Abril, Chenab Bridge).
MM1018 FL reaches ≥97% of design strength at 24 hours (+21°C) and full design strength at 7 days. Curing time can be accelerated with hot-air blowers, infrared spots, or heater blankets, up to a maximum accelerated-curing temperature of 50°C. Service load is not to be applied before strength is verified.
DIAMANT recommends grid-blasting to a roughness of 50-60 µm (SA2.5) where practical, and cleaning the surface free of oil and dust with DIAMANT cleaner or equivalent before injection.